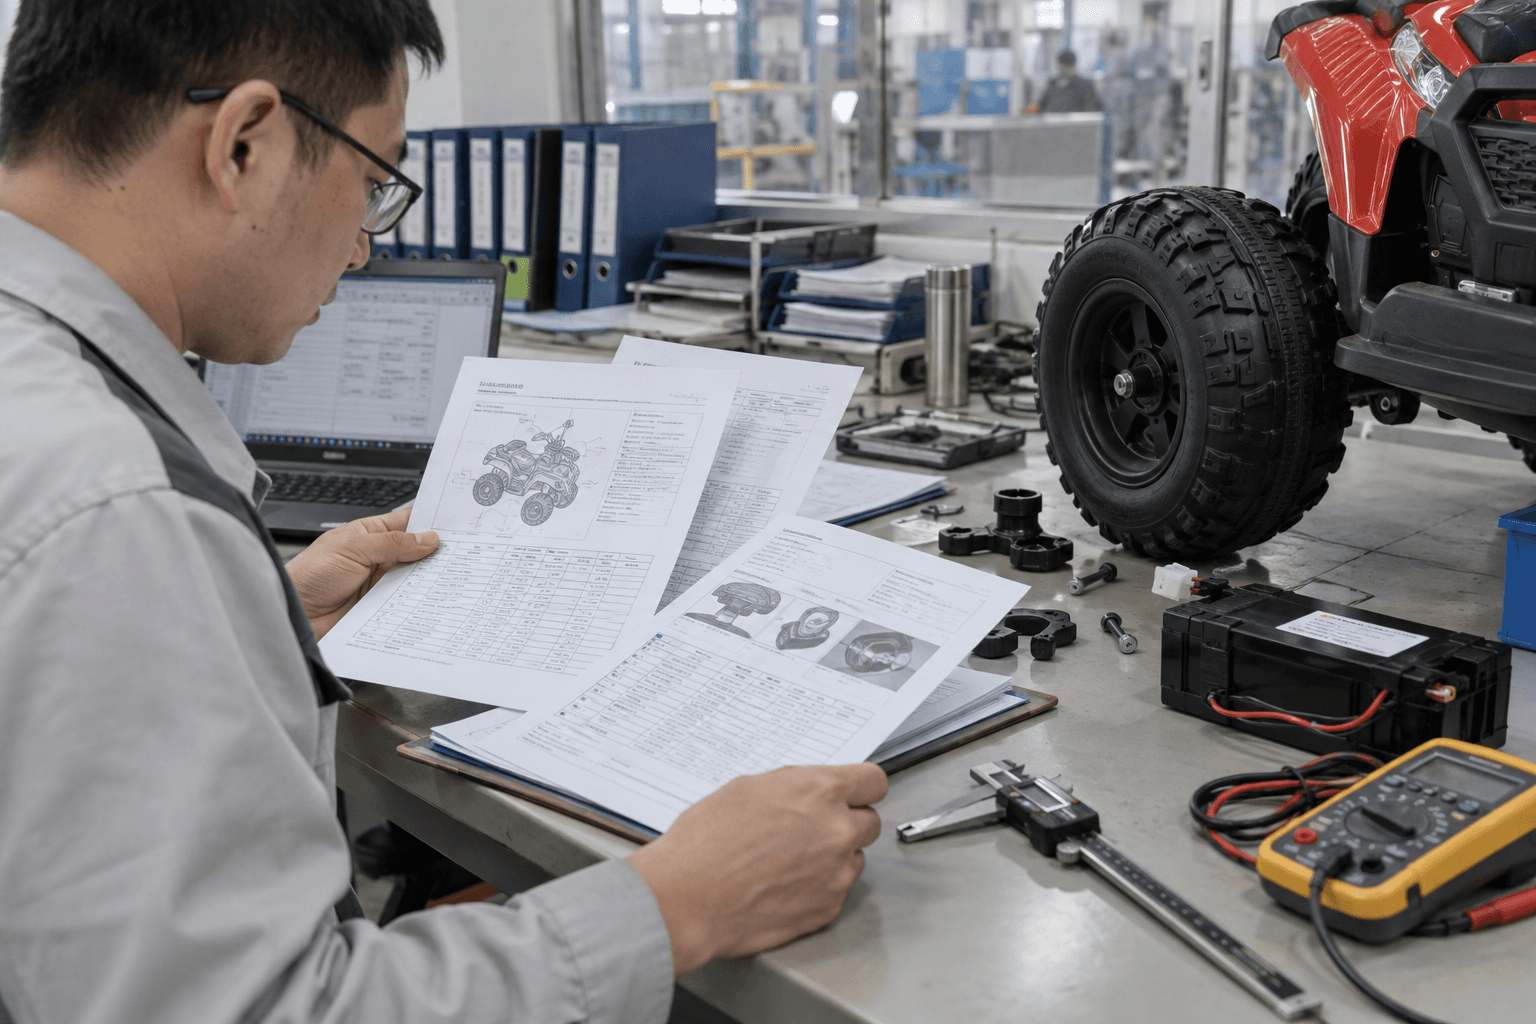
The short answer
Use a kids ATV design risk review to describe intended and foreseeable use, divide the product into functions and interfaces, identify failure modes, causes and effects, assess seriousness and uncertainty, specify design and process controls, plan validation, review residual risk and instructions, and maintain the analysis through changes. FMEA supports this work but does not replace required safety assessment or testing.
A list of parts is not a complete explanation of how a product can fail. The same connector can affect drive, charging, heat, service, or a stop function depending on where and how it is used.
This guide gives buyers a way to ask structured questions of qualified engineering and compliance teams. It does not provide a universal risk score or certify a design through a completed spreadsheet.
1. Start from the complete use and delivery journey
Describe receiving, unpacking, assembly, first charge, mounting, normal operation, turning, stopping, surfaces, supervision, cleaning, storage, service, transport, and disposal. Include foreseeable incorrect actions and interactions between the user, parent, retailer, and technician.
Use the intended rider and actual product configuration rather than a generic toy checklist. Review age, abilities, controls, vehicle mass, geometry, electrical system, accessories, and marketing claims. A foreseeable-use analysis can reveal risks that are invisible when teams inspect each part alone, such as charging a wet product or confusing a direction control during setup.
What to confirm before approval
- Map lifecycle states and responsible users.
- Include foreseeable misuse and service actions.
- Keep the configuration and intended user explicit.
2. Break the system into functions and interfaces
Identify what each subsystem must do: carry and restrain, steer, drive, slow and stop, charge, isolate electrical energy, indicate state, retain wheels, hold the battery, protect wiring, communicate instructions, and protect the product during shipment.
Review interfaces between subsystems, not only component quality. A correctly rated wire can still be pinched; an approved battery can be poorly restrained; a control can function but be misunderstood. Record the required function and performance boundary before listing failures. This gives the team a consistent reference for judging what has gone wrong and which evidence would demonstrate control.
What to confirm before approval
- Define functions before naming defects.
- Map mechanical, electrical, and human interfaces.
- Identify dependencies between controls and components.
3. Distinguish failure mode, effect, and cause
A failure mode describes what fails, the effect describes the consequence, and the cause explains the mechanism. “Motor does not run” is not the same as an open connector, and neither statement alone describes the possible consequences under different use states.
Use facts and plausible mechanisms. Consider occurrence, severity, exposure, detectability, and uncertainty according to the chosen method, but do not let a numerical score hide a serious hazard. Record assumptions and information gaps. A qualified team should review how the analysis relates to applicable rules, standards, foreseeable misuse, and required safety assessment rather than treating a low spreadsheet total as approval.
What to confirm before approval
- Use separate columns for mode, effect, and cause.
- Keep serious hazards visible regardless of score.
- Record uncertainty and required expert review.
4. Prefer effective design and process controls
Review whether the hazard can be removed or reduced by design, component selection, geometry, routing, restraint, guarding, control logic, error prevention, or validated assembly methods. Instructions and warnings remain important but should not compensate for an avoidable design weakness without proper assessment.
Assign each control to an owner and evidence method. A design measure may require engineering validation; an assembly measure needs process control; a service measure needs approved diagnostics and parts; a label requires placement and comprehension review. Distinguish prevention from detection. Finding a defect at final inspection is valuable, but preventing its creation may provide more reliable control.
What to confirm before approval
- Map each control to its failure mechanism.
- Separate preventive and detecting controls.
- Assign validation and implementation owners.
5. Connect the review with tests and physical evidence
Build a verification plan that identifies the configuration, condition, method, sample, equipment, result, and acceptance for each relevant question. Include qualified laboratory assessment where required and keep it distinct from routine line tests.
Use test failures to update the analysis rather than filing them separately. Record the observed mechanism, affected configurations, corrective change, and retest. If a test cannot reproduce a field issue, preserve that limitation and investigate use conditions, variation, or evidence quality. The absence of a failure in one test does not demonstrate the absence of every related hazard or remove the need for applicable compliance work.
What to confirm before approval
- Link each important question to evidence.
- Update failure analysis after findings.
- Keep laboratory and production-test scopes distinct.
6. Maintain the analysis through change and field feedback
Review new materials, component suppliers, software behavior, battery chemistry, tooling, geometry, accessories, packing, labels, and channels against the risk baseline. Connect changes to the first affected production batch and the updated test or document.
After launch, use complaints, returns, assembly confusion, inspection failures, and near misses to revisit assumptions. Ask whether the issue is isolated, whether existing detection should have found it, and whether other models share the same mechanism. A living review becomes part of design and quality decisions; an unchanged form archived after sample approval loses value as the product evolves.
What to confirm before approval
- Reassess meaningful product and process changes.
- Use complaint and production evidence.
- Review shared mechanisms across model families.
7. Worked example: apply the decision to a real order
The following scenario is illustrative. It explains a decision method rather than reporting a CubRover customer project, measured test result, certification, or completed shipment.
A team reviews a quad wiring route near a steering movement. The wire itself meets its specification, but assembly variation could place it where repeated steering creates abrasion.
The review separates the failure mode of damaged insulation, potential effects in relevant use states, and the causes of routing and retention variation. The team considers a different route, controlled retention, clearer work instructions, in-process verification, and suitable engineering validation. It then checks the updated process on representative production.
The worksheet is not the final proof. The evidence is the controlled design, effective assembly method, relevant tests, and continued production conformity. The example demonstrates structured reasoning and does not report an actual CubRover defect or establish a complete safety assessment for any model.
| Field | Question | Useful output |
|---|---|---|
| Function | What must the system do? | Measurable requirement |
| Failure and effect | What can fail and why does it matter? | Clear mechanism and consequence |
| Cause and control | How is the mechanism prevented or detected? | Assigned design or process action |
| Evidence | How is effectiveness demonstrated? | Validation and production records |
Questions to include in the buyer decision brief
Convert the review into questions that the supplier can answer against one named model and order. The following prompts come from the topic-specific approval checks above. They are intentionally practical: each answer should identify the responsible party, supporting record, open condition, and date by which the buyer can make the next decision.
- Start from the complete use and delivery journey: Map lifecycle states and responsible users. Include foreseeable misuse and service actions. Keep the configuration and intended user explicit.
- Break the system into functions and interfaces: Define functions before naming defects. Map mechanical, electrical, and human interfaces. Identify dependencies between controls and components.
- Distinguish failure mode, effect, and cause: Use separate columns for mode, effect, and cause. Keep serious hazards visible regardless of score. Record uncertainty and required expert review.
- Prefer effective design and process controls: Map each control to its failure mechanism. Separate preventive and detecting controls. Assign validation and implementation owners.
- Connect the review with tests and physical evidence: Link each important question to evidence. Update failure analysis after findings. Keep laboratory and production-test scopes distinct.
- Maintain the analysis through change and field feedback: Reassess meaningful product and process changes. Use complaint and production evidence. Review shared mechanisms across model families.
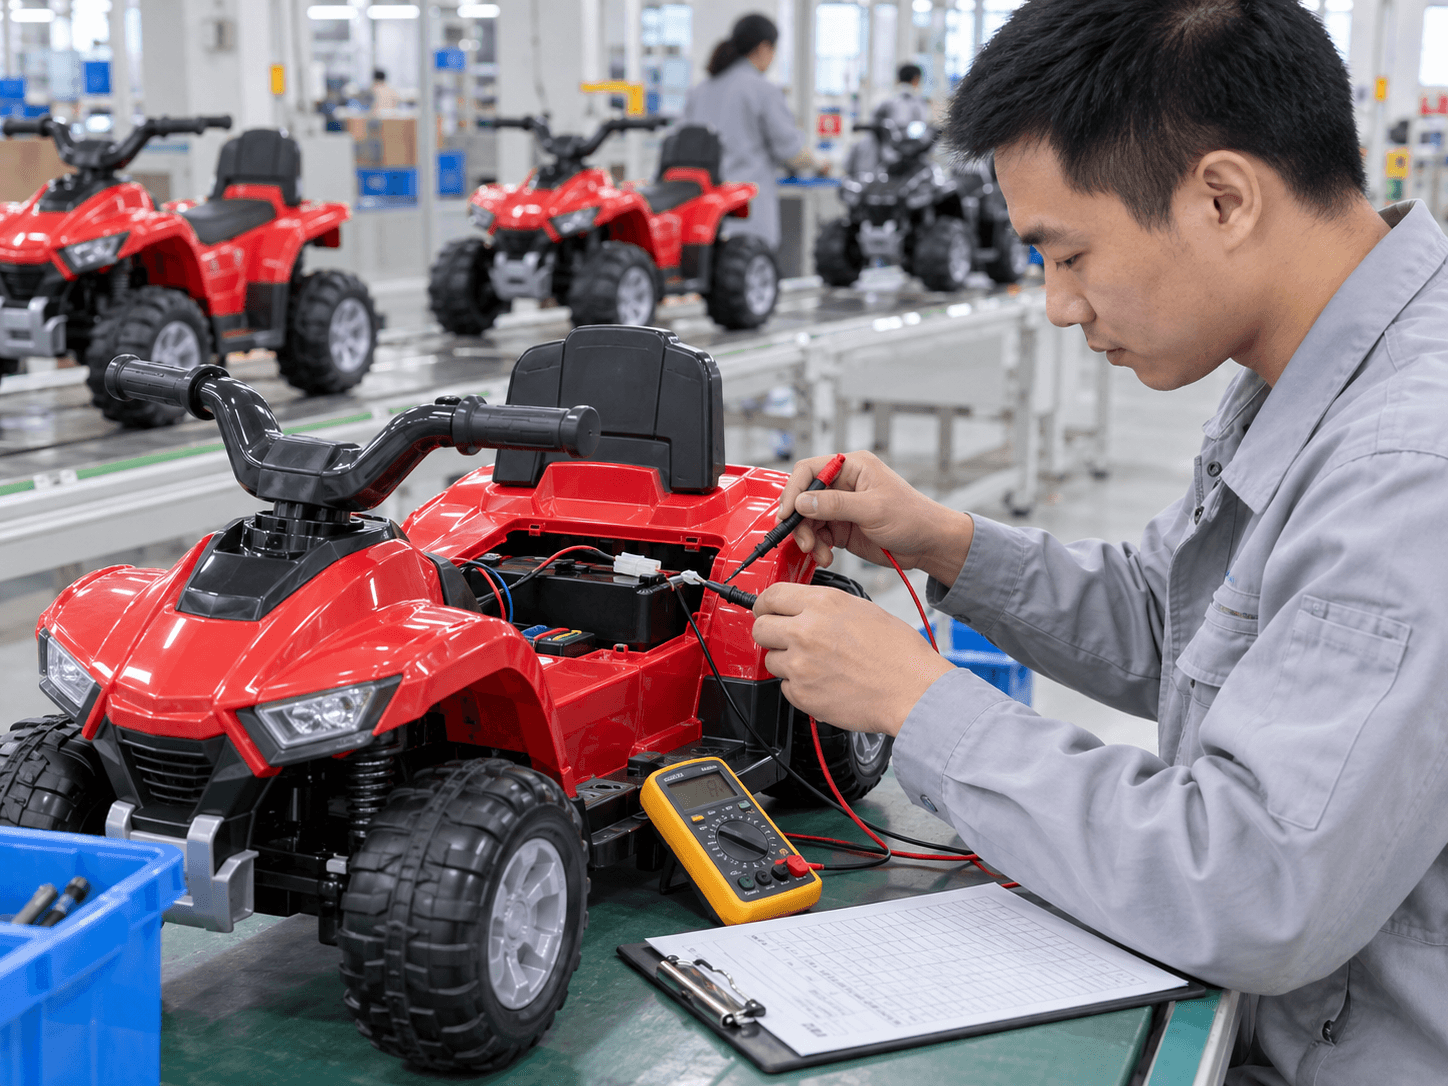
8. Turn the review into a controlled implementation plan
A useful buyer decision has three outputs: an approved requirement, evidence supporting that requirement, and a named person who can release the next activity. Keep these connected by model, configuration, market, document revision, and effective production date. If a supplier gives a conditional answer, preserve the condition in the purchasing record rather than shortening it into an unconditional product claim.
Ask for a focused multidisciplinary review involving product engineering, compliance, manufacturing, quality, service, and the buyer’s application knowledge. Keep decisions, open assumptions, validation tasks, residual risks, and change triggers tied to the model file rather than circulating a score without its reasoning.
- Define product functions and use states.
- Identify failures, effects, causes, and uncertainty.
- Assign effective controls and owners.
- Review relevant validation and residual risk.
- Maintain the analysis through production and field changes.
Agree evidence and acceptance before work starts
Write the review method before the sample, factory testing, document check, shipment inspection, or service exercise takes place. Specify the reference, sample selection, conditions, tools, result format, acceptance boundary, and response to a failure. This makes two quotations or results comparable and prevents teams from negotiating the meaning of a pass after money and time have already been spent.
Keep a compact, traceable decision file
Retain the original requirement, dated supplier response, model and component identity, relevant photographs, calculations, reports, deviations, approvals, and release decision. A screenshot can help communication, but retain the underlying record when it matters to the decision. Distinguish a proposed target from a measured value, an engineering sample from a production reference, and an internal check from a third-party assessment.
Use one current revision where possible. Purchasing, engineering, compliance, quality, logistics, sales, and service may need different views of the information, but they should not be making decisions from different versions of the product. When a change is approved, state the first affected batch and what happens to old materials, inventory, artwork, service parts, customer instructions, and pending shipments.
Review cost and timing together with product application
The lowest visible unit price may shift cost into testing, rework, freight, storage, retail setup, support, returns, or obsolete parts. Compare the complete customer requirement and the cost of supplying it consistently. Where a number is uncertain, show the assumption and a reasonable scenario range. Do not turn an illustrative calculation into a supplier promise or a universal benchmark for the category.
Reserve time for unresolved items. A sample modification may require another review; a component change may affect evidence; a carton revision may alter loading; a late document can affect handoff. Put the owner and decision date beside each open item. A useful schedule makes these dependencies visible instead of reporting one finish date that assumes every preceding decision will happen immediately.
Close the loop after delivery
After the first shipment or implementation, compare the approved assumptions with arrival condition, assembly preparation, actual costs, receiving accuracy, customer questions, service cases, and repeat-order results. Separate an isolated event from a recurring pattern using model, batch, channel, and time in use. When a discrepancy appears, contain the affected scope, identify the cause, implement the correction, and verify the next relevant outcome.
Primary resources for the specific source facts and frameworks discussed in this guide: CPSC toy-safety business guidance.
Continue the related CubRover buyer workflow: test-report coverage guide; complaint and CAPA guide; pilot production guide.
9. Conclusion and buyer handoff
A useful risk review explains functions, failures, effects, causes, controls, and evidence. Keep the analysis tied to real use, qualified judgment, product validation, process control, and the changing installed base.
Before requesting a quote, share the destination market, selected product platform, target quantity, required configuration, channel, timing, and the decision you need the supplier to support. Attach the current requirement and identify open questions. This gives the factory a clear starting point for discussing samples, evidence, inspection, documents, packaging, and commercial responsibilities.
Frequently asked questions
What does FMEA mean?
Failure Mode and Effects Analysis is a structured method for reviewing potential failures, their effects, causes, and controls.
Does an FMEA replace safety testing?
No. It supports design and quality decisions alongside applicable assessment, standards, validation, and tests.
Is a low risk score proof of safety?
No. Scoring depends on the method and assumptions; serious hazards and uncertainties need explicit expert review.
Who should join the review?
Relevant engineering, compliance, manufacturing, quality, service, supplier, and buyer application representatives.
Should warnings be the first control?
Review effective design and process measures as well as instructions under qualified risk assessment.
When should the review be updated?
After relevant design, component, process, market, use, test, inspection, complaint, or service evidence changes.
Connect development questions with evidence
Discuss the exact configuration and validation needs with CubRover.
Contact Us